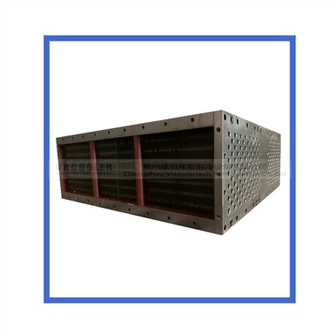
Shell And Tube Heat Exchanger in A Chemical Plant Project
Use case: Shell and Tube Heat Exchanger in a Chemical Plant Project
Project Background:
In a chemical plant in Germany, high-efficiency heat transfer was required to increase the efficiency of the production process and reduce energy consumption. High-temperature waste heat from the chemical plant's production process needed to be recovered and utilised, while the new production process required a reliable cooling system.
Design Specifications:
Heat exchanger type: Shell and tube heat exchanger
Material: Stainless steel shell and tube bundle to resist chemical corrosion
Heat transfer area: 150 square meters
Design temperature: 80°C (hot side), 25°C (cold side)
Design pressure: 1.6 MPa (shell side), 1.0 MPa (tube side)
Fluid medium: High-temperature waste heat generated in the chemical process
Project Situation:
Shell and tube heat exchangers were designed and integrated into the production process of this chemical plant. With the shell and tube heat exchanger, waste heat is recovered for preheating the fresh feed to provide the required heating and cooling in the production. The system operates stably in the high temperature, high pressure, and corrosive environment of the chemical plant, providing reliable heat recovery and cooling.

Customer Feedback:
Customers are delighted with the performance and reliability of the shell-and-tube heat exchanger. They said that the shell and tube heat exchanger not only excelled in providing high-efficiency heat transfer but also showed excellent resistance to the harsh working environment of the chemical plant. The high waste heat recovery rate saves them a lot of energy expenses, making the production process more environmentally friendly and economical. The customer appreciated the heat exchanger's design, build quality, and the service provided, and they plan to extend similar systems to other production lines.